TaC Coated Susceptor Factory Quality Standards Buyers Should Evaluate
2026-11-16
Sourcing TaC coated susceptors is rarely just a purchasing decision; it is an investment in wafer uniformity, tool uptime, and repeatable epitaxial performance. However, many buyers overlook the factory-level quality controls that determine whether a susceptor will survive thermal cycling, aggressive cleaning chemistries, and high-volume production without early coating degradation. Before comparing quotes, it is worth looking beyond surface finish and dimensional reports. This guide breaks down the practical quality standards buyers should evaluate when selecting a TaC coated susceptor factory, with insights aligned to Semicorex manufacturing and inspection practices.
Raw Graphite Grades That Make or Break TaC Adhesion
TaC adhesion rarely fails because of the coating alone. The graphite grade underneath sets the ceiling. Fine-grained, high-density isotropic grades with low open porosity tend to produce the most stable bond. Their tight structure limits outgassing and gives the TaC layer a consistent thermal expansion partner. Coarse extruded grades with large, visible filler particles often create local stress points, and the irregular surface makes it harder for the coating to bridge gaps without micro-cracks.
Purity matters just as much as grain structure. Trace metallic impurities and residual ash in lower-cost graphite can migrate during high-temperature deposition and form weak interfacial compounds. Those compounds may look fine after coating but delaminate after thermal cycling. Grades with controlled ash content and higher graphitization temperatures usually provide a cleaner, more stable surface for TaC to anchor to.
Even the best raw graphite can be undermined by machining, but the wrong base grade cannot be fixed by surface prep. Opening pores or exposing binder-rich areas during milling creates variable surface energy, which encourages uneven nucleation. Choosing a grade that matches the coating process rather than treating graphite as a passive substrate is often what separates a coating that lasts from one that flakes off after a few cycles.
Coating Thickness Verification Beyond the Certificate
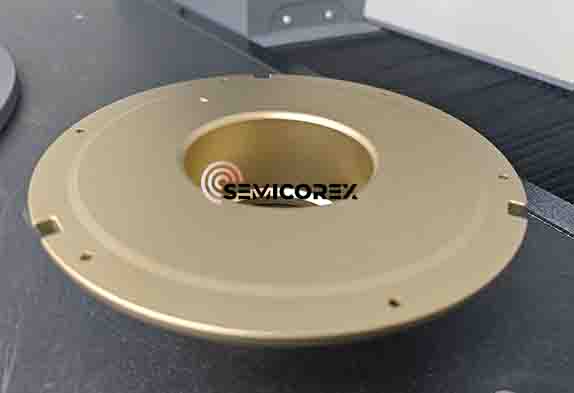
A certificate tells you the coating thickness was measured at a handful of spots, often under ideal conditions and on a clean, flat surface. What it rarely captures is what happens on the actual structure: edges that pull coating thin, welds with rough profiles, inside corners where spray patterns struggle, and areas that were touched up after assembly. Verifying thickness beyond the certificate means walking the job with a calibrated gauge and checking the places the paperwork never mentions.
The real question is not whether the average reading meets the spec, but whether the low readings fall outside it. Most standards allow a limited number of spot measurements below nominal thickness, but they also set a minimum that no single reading should drop below. On complex geometries, that minimum is where failures hide. Rust, premature coating breakdown, and warranty disputes often trace back to a small patch that was never measured because it was inconvenient to reach.
Beyond the gauge, verification involves looking at the surface condition under the coating, the dry film thickness around fasteners and cut edges, and the consistency across different applicators and shifts. It means comparing the certificate to the actual batch numbers, recoat windows, and cure conditions. When the paperwork and the structure disagree, the structure always wins.
Thermal Cycling Tests That Predict Early Peeling
Peeling failures usually begin well before they become visible. At a bonded or coated interface, each temperature swing creates a mismatch in expansion that acts like a slow pry bar. Thermal cycling tests turn that mechanism into a controlled sequence, alternating between a cold soak that embrittles the surface layer and a hot dwell that softens it. The repeated strain does not just check adhesion; it gradually opens micro-channels where oxygen and moisture can reach the interface, making the test a useful early warning system.
The profile design matters more than the total number of cycles. A ramp that is too fast can tear the sample artificially, while a dwell that is too short may not allow the substrate to reach thermal equilibrium. In practice, a test becomes predictive when the cycle includes enough time at the extremes for stress relaxation to occur, because that is when interfacial bonds start to fatigue in the same way they would outdoors. Sudden edge lifting around fasteners or cut edges after relatively few cycles often correlates with early-field peeling long before coating removal becomes widespread.
Reading the results properly means tracking the onset of microscopic changes rather than waiting for large-scale delamination. Blister count, edge creep, gloss variation, and changes in pull-off force can all shift earlier than the visible peel line. By recording these indicators at fixed intervals, a thermal cycling program can distinguish a coating or adhesive that will remain intact from one that is only temporarily passing a single adhesion check.
Inspecting Pocket and Edge Finish Before Shipping
Before anything gets sealed into a polybag, I turn each piece inside out and run my fingers along the pocket seams. A pocket can look fine on the surface and still hide a broken stitch, a skipped needle, or lining that twists just enough to make the opening pull awkwardly. I check both corners twice because that's where tension tends to gather and small tears start.
Edge finish gets the same slow once-over. Whether the edge is bound, folded, or painted, it has to sit flat with no bubbles, cracks, or sticky residue. I'll compare the edge tone against the main fabric under the same light we use for final inspection, not just by the cutting table, since a mismatch becomes obvious later in daylight or under store lighting.
The last pass is about how a customer would actually see it. I open each pocket partway, let the fabric relax, and check that the mouth doesn't gape, curl, or show raw edges from a normal angle. If something catches my thumb or looks uneven at arm's length, it goes back for correction instead of into the shipping carton.
Supplier Batch Records Worth More Than a Clean Spec Sheet
The spec sheet might list every additive, every micron rating, every cure time—but it rarely tells you what actually happened on the floor. Supplier batch records are the difference between a promise and a paper trail. They capture the raw material lots, the machine settings, the operator notes, the mid-run adjustments, and the occasional anomaly that never makes it into marketing copy. If you are buying critical components, those records matter more than the glossy one-pager.
A clean spec sheet implies consistency. A detailed batch record proves it. When something drifts out of tolerance weeks or months later, the spec sheet will not help you trace the root cause. The batch record will. It shows whether the supplier caught the deviation, how they handled it, and whether they quietly shipped it anyway. That is the kind of visibility that separates a vendor from a long-term partner.
Think of it this way: anyone can write a target value on a PDF. Very few can hand over the actual history of every production run and stand behind it. Ask for batch records before you need them. If a supplier hesitates, that hesitation tells you more than any certificate of conformance ever will.
What Protective Packaging Reveals About Quality Control
Protective packaging is often treated as an afterthought, but it's one of the clearest outward signs of how a company handles defects. A business that chooses the right insert depth, pairs the box size to the product rather than whatever is nearby, and seals with care is usually running checks that extend far beyond the shipping table. When foam is pre-scored to match the item or corner boards are placed exactly where stress will hit during transit, it means someone studied real failure points instead of copying a generic packing list.
The less obvious signals matter just as much. Consistent tape length, clean film layers, and void fill that stays put without being overstuffed all point to a packing line with standard work instructions and someone accountable for the last few feet of the process. If packaging varies wildly from one order to the next—torn edges, uneven wrap tension, labels slapped at random—that variability typically travels backward into assembly, inspection, and supplier management.
Material decisions are another quiet tell. Moisture barriers, anti-static wraps, and reinforced seams don't appear by accident; they reflect a team that has mapped out what can go wrong between the dock and the customer's hands. When those choices are consistently applied, they suggest the same preventive mindset that keeps rejects from leaving the facility in the first place.
FAQ
Demand evidence of repeatable runs across full-size parts, not just coupon samples. A factory should show control over gas flow, temperature gradients, and deposition time so the TaC phase stays consistent and free of unconverted carbon or metallic residues across the entire working surface.
Ask for cross-hatch or scratch test data combined with thermal cycling results between room temperature and at least the upper use temperature. The real test is whether the coating survives repeated expansion and contraction without cracking, peeling, or exposing the graphite base.
Look for suppliers that use eddy current, beta backscatter, or calibrated ultrasonic mapping rather than a single spot check. Pocket edges, rims, and curved transitions need separate measurement points because those are the first places where uneven coating creates hot spots or early erosion.
The exact limits depend on the epi process, but a reasonable starting point is to require low single-digit ppm or better for critical transition metals like Fe, Ni, Cu, and Cr, with data from GDMS or ICP-MS on finished coated parts rather than raw powder certificates alone.
Roughness affects wafer temperature uniformity, particle generation, and even how residues clean off between runs. A polished TaC surface with controlled Ra alone is not enough; the texture also needs to be non-porous and free of grinding marks that trap contamination.
Ask how parts are cleaned, dried, and packed after final inspection. Reliable facilities use controlled environment packaging, gloves and face masks during handling, and individually sealed containers that prevent graphite dust or plastic fibers from reaching the coated surface before installation.
Request run charts for thickness, density, surface roughness, adhesion test values, and final dimensional inspection across at least three to five production lots. This shows whether the process is stable or whether the supplier is selecting only the best samples for qualification.
Measure pocket diameters, depths, overall flatness, and the fit of any locating features after coating. Because TaC adds thickness and high-temperature operation changes graphite dimensions slightly, the buyer should confirm that the coated part meets the drawing in its final state, not just the machined graphite blank.
Conclusion
A TaC coated susceptor is only as reliable as the graphite underneath it. Buyers should press suppliers on the specific raw graphite grade, grain size, and impurity profile, because a cheaper blank often leads to uneven coating adhesion and early flaking even when the certificate looks acceptable. Thickness data on paper means little unless the factory can show measurements taken at multiple points across pockets, sidewalls, and edge transitions, not just one favorable spot. Thermal cycling evidence matters just as much; a supplier that cannot walk you through repeated heating and cooling runs is unlikely to catch stress points that turn into peeling after a few hundred production cycles.
Close inspection before shipping should include pocket corners, chamfers, and edge breaks, since rough or inconsistent finishing creates stress risers under process conditions. Batch records tell a more honest story than a polished specification sheet: look for raw material lot numbers, coating furnace logs, thickness readings, and rejection history tied to each susceptor. Packaging is another quiet signal of factory discipline. If susceptors arrive with loose foam, exposed edges, or generic crates, the same carelessness probably exists in earlier process steps. A supplier that protects the finished surface with sealed, labeled, and traceable packaging is usually the one that controls the less visible stages as well.
Contact Us
Contact Person: Svenja Wei
Email: [email protected]
Tel/WhatsApp: +8613567891907
Website: https://www.semicorex.com