PTFE Gasket Exporter Checklist for Quality Assurance and Compliance
2026-10-27
Every seasoned importer knows the real cost of a PTFE gasket isn’t the unit price—it’s what happens when quality or compliance slips through. A delayed container, a failed audit, or a chemical incompatibility can erase months of hard-won trust. That’s why a focused pre-shipment checklist matters more than ever. At TAIFNO, we’ve built our export process around hard checks, not assumptions: material purity, dimensional tolerances, chemical resistance, and full documentation traceability. In this post, we’re sharing the exact checklist we use to keep every shipment compliant and every client confident.
Checking Raw Material Certificates Against Order Specs
Mismatches between raw material certificates and order specifications are caught before anything reaches the production floor. The cert is read line by line against the purchase order, focusing on alloy grade, dimension, heat number, and any supplementary requirements like impact testing or fine grain practice. If the mill cert lists a yield strength below what the order asks for or the chemistry drifts outside the allowed range, the material is set aside and the supplier is contacted immediately.
Attention also goes to the certificate's issue date and the standard revision. Older certs sometimes reference versions of ASTM or EN standards that have since been updated, and that alone can make the material nonconforming. Handwritten corrections or altered values on the cert trigger a closer review before the heat is accepted. This step is not about paperwork for its own sake; it is the last clear chance to stop a wrong grade from being cut, welded, or machined into a finished part.
Verifying Dimensional Accuracy Before Packing
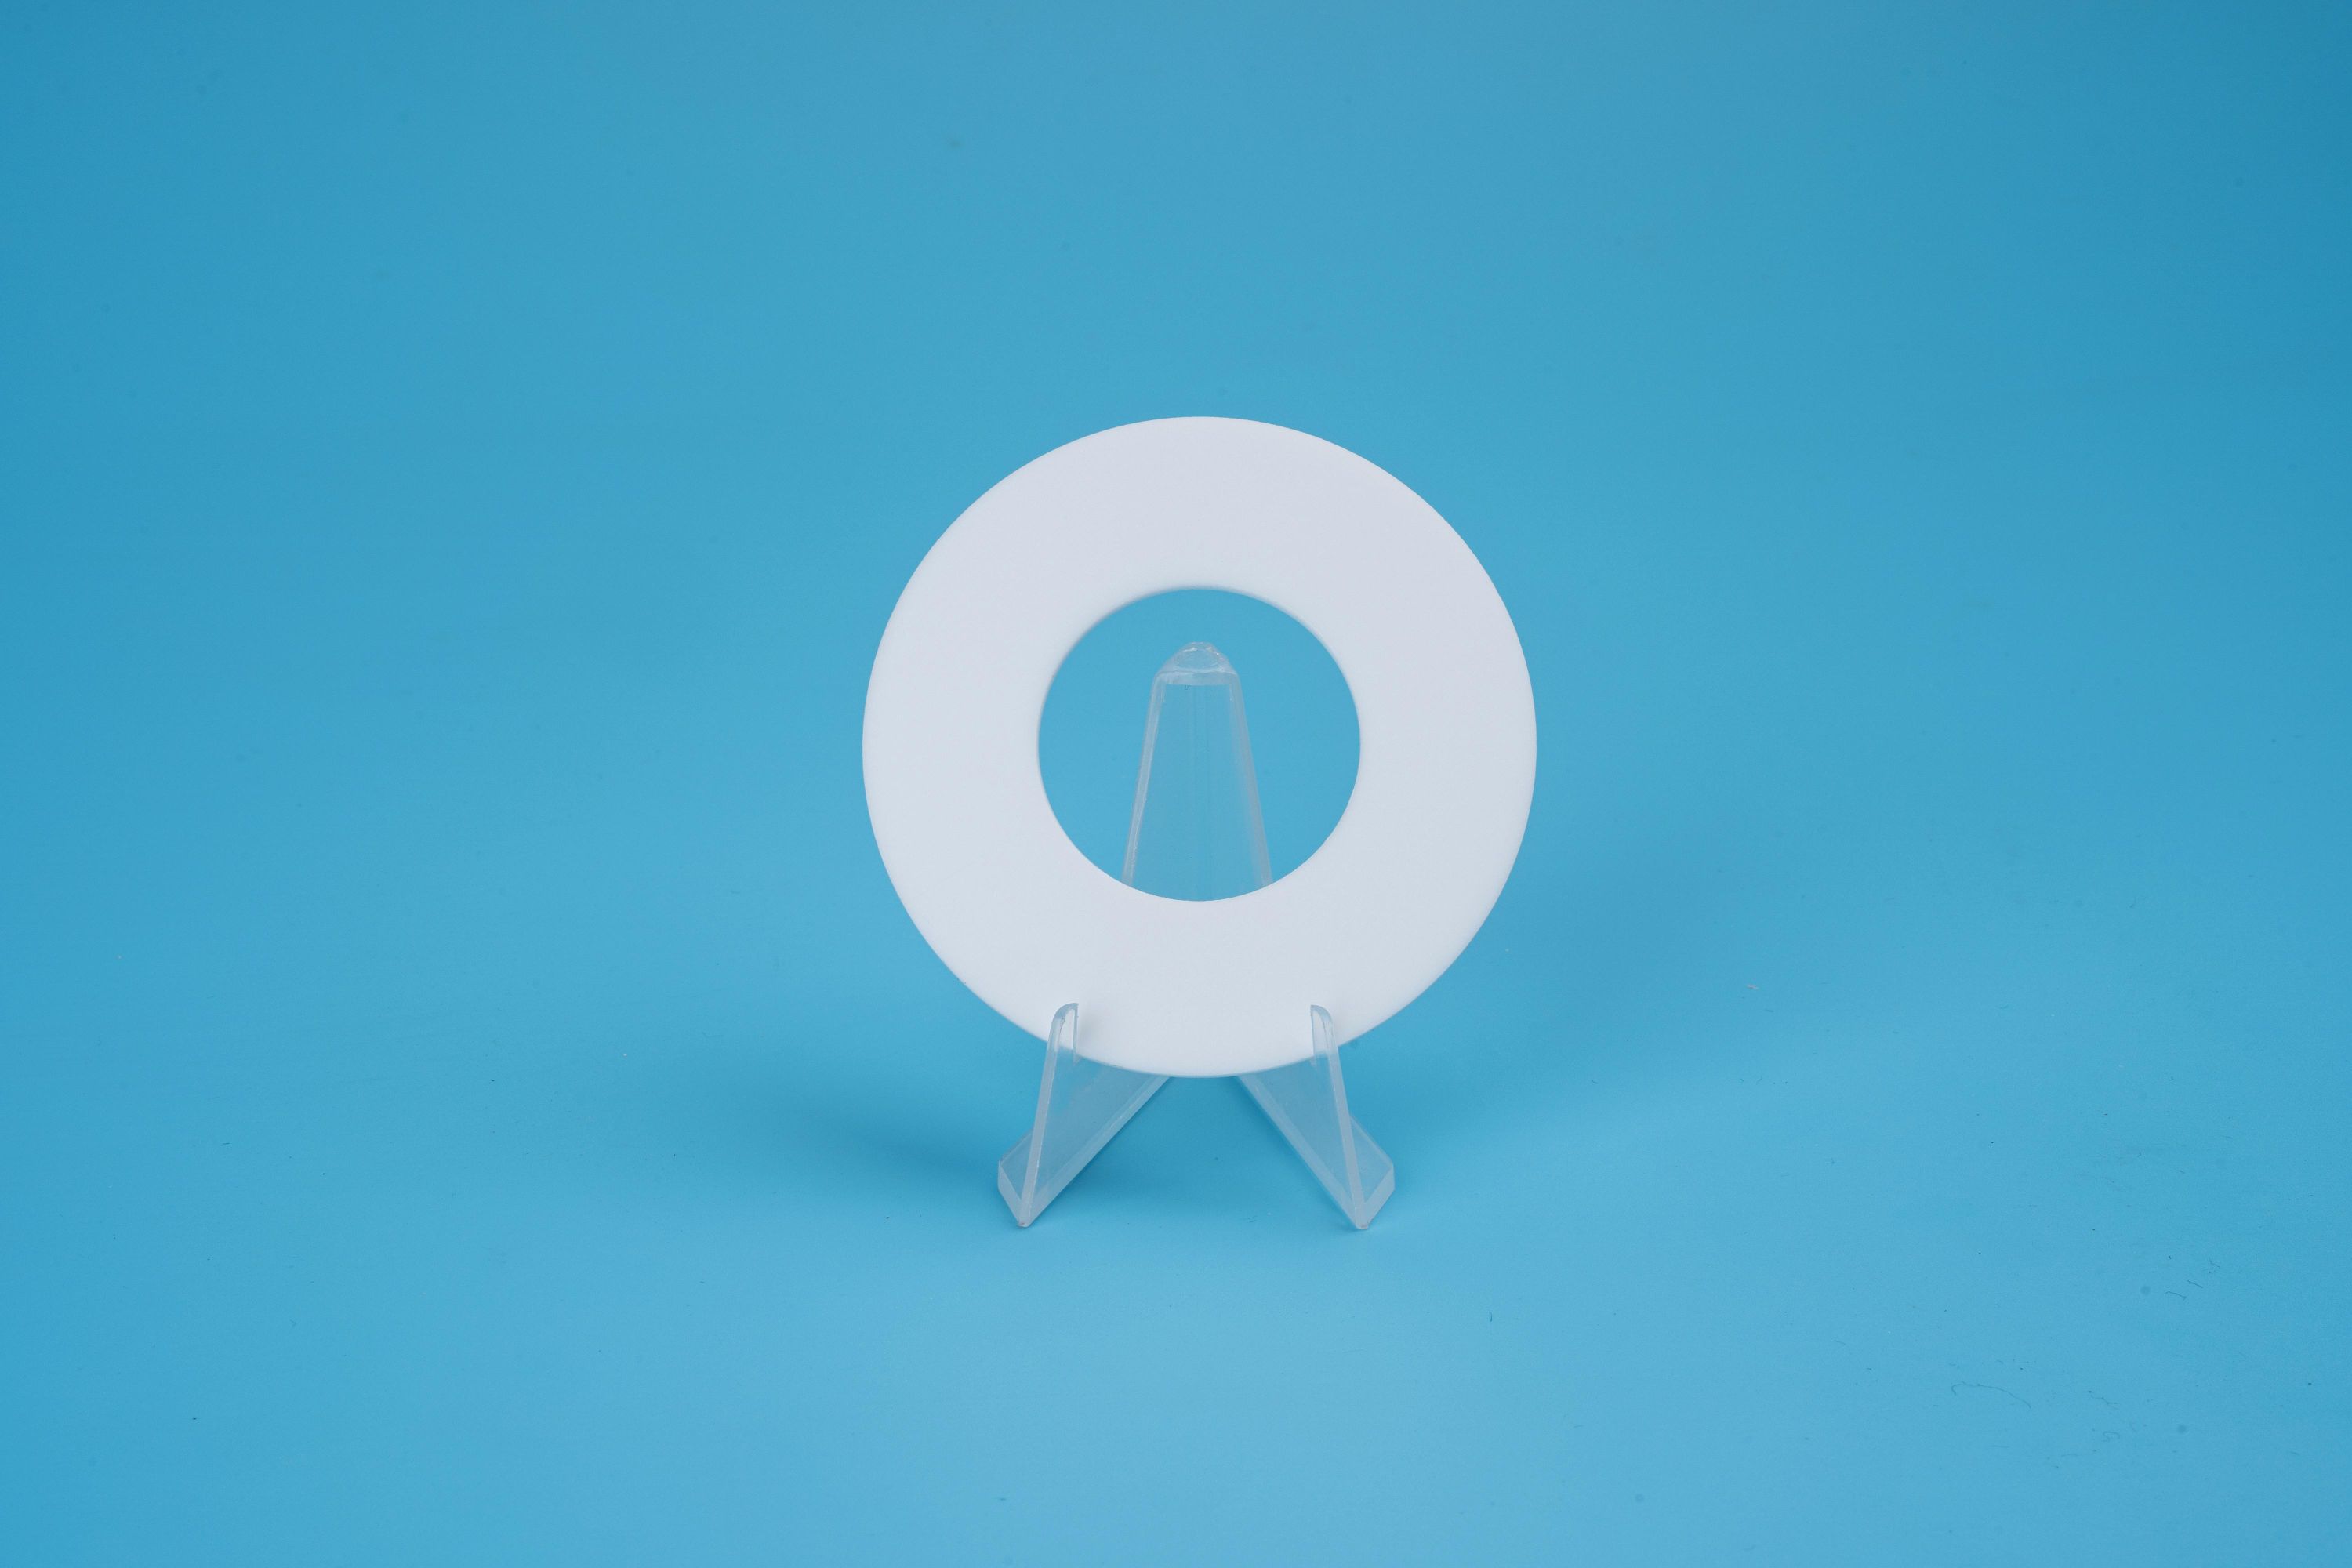
Dimensional checks before packing work best when they follow a short list of agreed critical dimensions rather than a random sweep. For parts with a tolerance of ±0.05 mm or looser, a calibrated caliper is usually enough. Tighter tolerances call for a micrometer, a bore gauge, or a bench fixture that holds the part the same way every time. After the first-off part is approved, the operator should recheck those same dimensions at a fixed interval, such as every 20 or 30 pieces, not just when something feels wrong.
How the part is supported during measurement matters as much as the instrument itself. A thin-walled housing or a long bracket can flex under its own weight, so take the reading with the part resting on a flat surface or in a purpose-made nest. If a go/no-go gauge is used, apply only light finger pressure; forcing the gauge can mask an undersized feature. Record actual readings instead of writing only "OK" or "NG." The numbers show drift early and make it easier to trace a problem back to a specific cavity, tool, or shift.
A final dimensional spot check just before packing is also a good moment to account for temperature. Plastics and aluminum move more than steel with small room-temperature changes, so a part that measures in spec at the machine may sit slightly over limit after cooling near an open dock door. If a dimension lands close to the upper or lower tolerance, do not simply release the batch. Recheck the process stability or measure a larger sample before sealing the carton.
Running Pressure and Leak Tests on Finished Gaskets
Once a gasket is cut or molded, it has to prove itself under conditions close to real service. The finished part is typically clamped between blind flanges or a dedicated test rig that reproduces the actual bolting pattern and flange surface finish. A common starting point is a hydrostatic pressure test at 1.5 times the design pressure, held for a set duration while dial indicators and close visual checks monitor for any pressure drop, weeping, or distortion around the seating area.
Leak detection goes beyond looking for drips. For gas services, a soap film bubble test can expose pinholes that water pressure alone might miss. More critical joints often call for helium mass spectrometry, where a tracer gas is introduced on one side and a sniffer probe or vacuum chamber measures the escape rate down to 10^-6 mbar·L/s or tighter. The chosen method depends on the gasket material, the fluid it will seal, and how unforgiving the application is.
A pass is not just about zero visible leakage. The gasket also needs to recover elastically after pressure is removed, so thickness readings are taken before and after the cycle to confirm creep relaxation stays within the manufacturer's limits. Any misalignment in the fixture or uneven bolt preload can make a good gasket look like a failure, which is why the test rig itself gets calibrated and inspected before each run.
Aligning Packaging Labels With Import Country Rules
Aligning packaging labels with import country rules rarely means simply swapping one language for another. A product sold in the Gulf Cooperation Council states may require Arabic text in a minimum font size alongside English, while the same item entering Canada demands metric-only net quantity declarations and French labeling if it reaches Quebec. Even symbols that look universal—recycling codes, use-by icons, caution marks—can carry different legal weight from one customs territory to the next. Mapping these requirements early avoids treating compliance as a last-mile translation task.
The real cost of misalignment shows up at the border, not on the shelf. A shipment held for a missing importer address or an outdated pictogram can trigger demurrage charges, forced relabeling, or outright rejection. Importers often discover that a distributor's label review is not a substitute for local regulatory confirmation. Building a checklist tied to each destination market—covering label dimensions, language order, hazard phrasing, and country-of-origin wording—turns a fragmented risk into a repeatable process.
One practical approach is to design a label architecture with fixed and variable zones. Brand elements, product identity, and barcode placement stay stable across markets, while the variable zones absorb country-specific text, symbols, and legal identifiers. This keeps visual consistency without forcing every export to carry the same regulatory burden. Updating the artwork becomes faster when a change in one market does not require rebuilding the entire label for all destinations.
Confirming Chemical Resistance Claims With Lab Reports
Chemical resistance ratings advertised by material suppliers often rest on standardized tests performed under ideal conditions. Actual service environments, however, introduce variables such as temperature swings, concentration fluctuations, and mechanical stress that can shift a material's performance beyond the scope of a generic compatibility chart. Without reviewing the original lab reports, buyers are left trusting a claim rather than verifying the data behind it.
A meaningful confirmation process starts by requesting documentation that names the exact test method, exposure duration, and chemical concentration used. Look for details like whether the material was under load during immersion or if post-exposure properties such as tensile strength or hardness were measured, not just visual appearance. Reports from third-party facilities accredited to ISO 17025 carry more weight than in-house summaries, because they follow documented procedures and include uncertainty ranges.
When comparing options, ask suppliers to map their test conditions to your operating parameters. A material that survives 98% sulfuric acid at room temperature may fail rapidly at 60°C with intermittent exposure to air. Requesting the raw data, not just a pass/fail verdict, allows you to spot marginal results that could become field failures under cyclic conditions. This level of scrutiny separates vendors who truly understand chemical compatibility from those who simply repeat catalog language.
Pre-Shipment Document Review to Prevent Customs Holds
Mistakes in paperwork are one of the most common reasons shipments get stuck at the border. A careful pre-shipment document review checks every detail—commercial invoice, packing list, certificate of origin, and any required permits—against the actual goods and the destination country's rules. Even a small mismatch, like a missing HS code or an inconsistent weight, can trigger a hold that costs days of storage and frustrated customers.
Beyond basic accuracy, this step also flags red flags that customs officers look for: vague product descriptions, undervalued goods, or missing importer information. By cross-referencing the documents with the purchase order and the carrier's manifest, you can catch discrepancies before the cargo leaves the warehouse. This proactive approach turns a simple checklist into a safeguard against delays, fines, and unexpected return shipments.
For teams handling multiple suppliers, a standardized review process makes all the difference. Assign clear ownership—someone who knows both the product and the destination's import requirements. Use a short, practical checklist that evolves with real-world customs feedback. You'll not only reduce holds but also build a reputation for reliable delivery, which keeps clients coming back.
FAQ
Ask for the resin manufacturer's certificate of analysis showing virgin PTFE grade, not reprocessed or blended material. The certificate should list tensile strength, elongation at break, density, and particle size. For food or pharma applications, also request a statement of compliance with FDA 21 CFR 177.1550 or EU 10/2011. If the supplier only provides a generic COA, request batch-specific traceability documents that tie the resin lot to the finished gasket lot.
Many inspectors only check outer diameter and thickness, but skip inner diameter concentricity and bolt hole positioning. PTFE flows under load, so check thickness at multiple points around the circumference, not just one spot. Also verify flatness with a feeler gauge on a granite surface plate—warped gaskets can cause uneven compression. For ring gaskets, measure the cross-section width in at least four places to catch out-of-round conditions.
Keep a technical file for each gasket compound that includes the resin supplier's EU 10/2011 declaration and migration test data. Then you can issue your own declaration of compliance for each shipment, as long as the compound and production process haven't changed. For high-risk applications, do periodic migration testing on finished gaskets—not just on the resin—because fillers like glass or barium sulfate can affect overall migration limits.
Beyond the commercial invoice and packing list, include a batch test certificate with actual results, not just a statement saying 'passes.' Add a material safety data sheet if the gasket contains fillers, a certificate of origin, and a packing declaration for wooden crates if applicable. For markets like the Middle East, a pre-shipment inspection certificate from a third party is often mandatory. Also include a digital copy of the gasket drawing with revision number so customs can match the part to the invoice.
Never stack large-diameter PTFE gaskets flat without support. Place them vertically in partitioned crates or hang them from the center hole using non-metallic pegs. For smaller gaskets, lay them in single layers between foam sheets inside rigid boxes. Avoid using plastic wrap directly on the gasket surface—PTFE can pick up static charge and attract dust. Seal the final package with desiccant packs and a humidity indicator card if the destination has high moisture.
Creep relaxation depends on filler content, but for virgin PTFE, a loss of more than 40% of initial bolt load after 24 hours at 100°C is a red flag. For filled PTFE with glass or carbon, aim for less than 30% loss. The test method matters—ASTM F38 Method B is common for sheet gaskets. Exporters should test at the actual service temperature promised to the buyer, not just room temperature, because virgin PTFE softens dramatically above 150°C.
First, quarantine the entire batch and review the production records for that day—check the compression molding pressure, sintering cycle, and cooling rate. A leak failure with no visible defect often points to micro-porosity from too-rapid cooling or trapped air in the preform. Cut open a few samples and inspect under magnification for internal voids. If the root cause is found and isolated, rework may be possible by re-sintering, but never ship the batch with a 'borderline pass' note—importers will return it.
Record the resin lot number, filler batch if used, mixing time and temperature, mold number, press operator, sintering oven profile with actual temperature chart, and final inspection results. Link all this to a unique lot code stamped on the gasket or its packaging. This allows you to trace a field failure back to a specific resin batch or oven cycle within hours. Without it, a single customer complaint can force a recall of every shipment made in that quarter.
Conclusion
Quality assurance for PTFE gasket exports starts well before production wraps. Every incoming batch of raw material is cross-checked against the customer's purchase specification—certificates are not taken at face value, and any mismatch flags the lot for quarantine. Once blanks are cut or molded, dimensional checks become non-negotiable; a gasket that drifts outside tolerance on inner diameter, outer diameter, or thickness can compromise flange sealing even if it looks fine on a shelf. Finished pieces then move through pressure and leak testing, typically with compressed air or nitrogen under controlled conditions, to confirm they hold integrity at rated operating limits. Alongside this, chemical resistance claims are validated with up-to-date lab reports from accredited third parties, because a PTFE grade that works in one acidic environment may fail in another solvent or high-temperature application. These steps turn a simple product checklist into a defensible quality record rather than a box-ticking exercise.
On the compliance side, packaging labels require more than a generic part number. Import country rules can dictate language, hazard symbols, batch traceability, and even the placement of country-of-origin marks; exporters who reuse domestic labels often face rejected shipments at the port. Each carton is therefore reviewed against the destination market's current labeling directives before sealing. In parallel, the pre-shipment document pack—commercial invoice, packing list, certificate of origin, mill test reports, and any buyer-specific declarations—is audited line by line. Discrepancies between the invoice weight and the actual packing list, or a missing conformity certificate, are common triggers for customs holds. A final reconciliation of physical goods, labels, and paperwork acts as an export gate: nothing leaves the dock until every requirement lines up. This second layer of checks protects both delivery timelines and the exporter's reputation, and it turns compliance from an afterthought into a scheduled part of the shipping workflow.
Contact Us
Contact Person: Tommy Xiao
Email: [email protected]
Tel/WhatsApp: 8615651509888
Website: https://www.ptfe-factory.com